Another (but expensive) option is the Parmakit crank for their 'sixty six' 205cc kit for the 125/150 motor. I think the case still needs some fettling for this option:
https://www.vespatime.it/en/engine-parts/crankshafts/crankshaft-advanced-parmakit-vespa-px-pe-125-150-stroke-60-connecting-rod-110.2.20.100.gp.6109.uw
|
|
|
Nedminder

62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
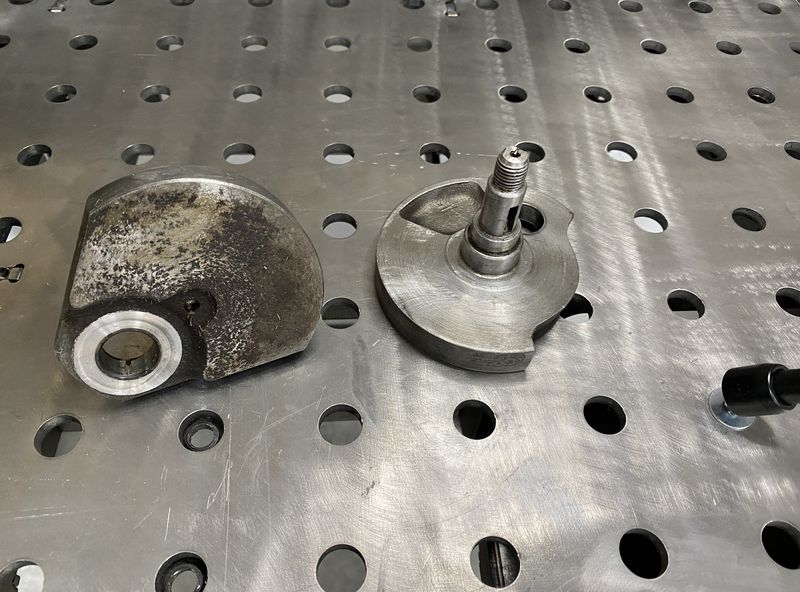
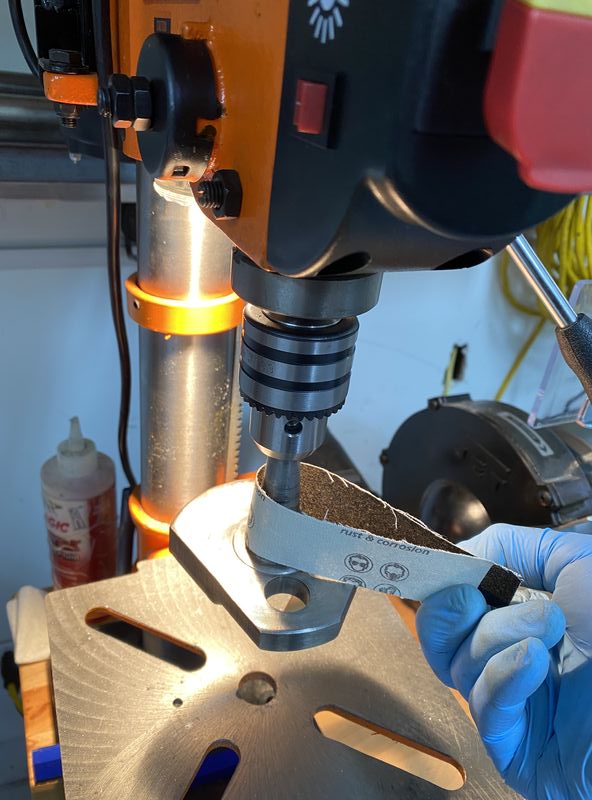
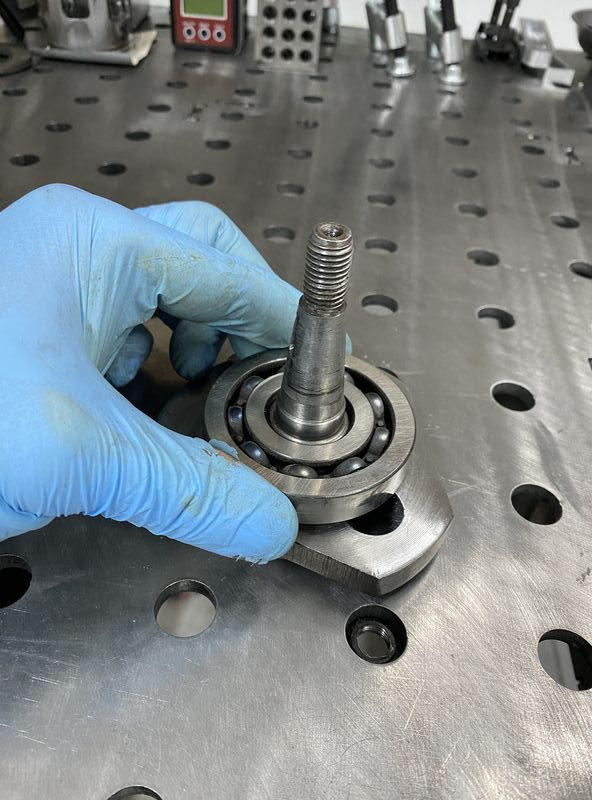
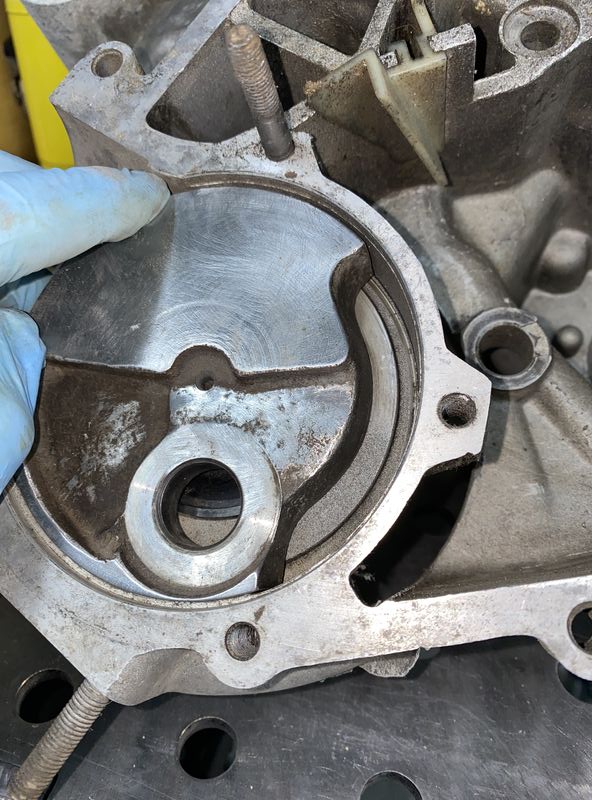
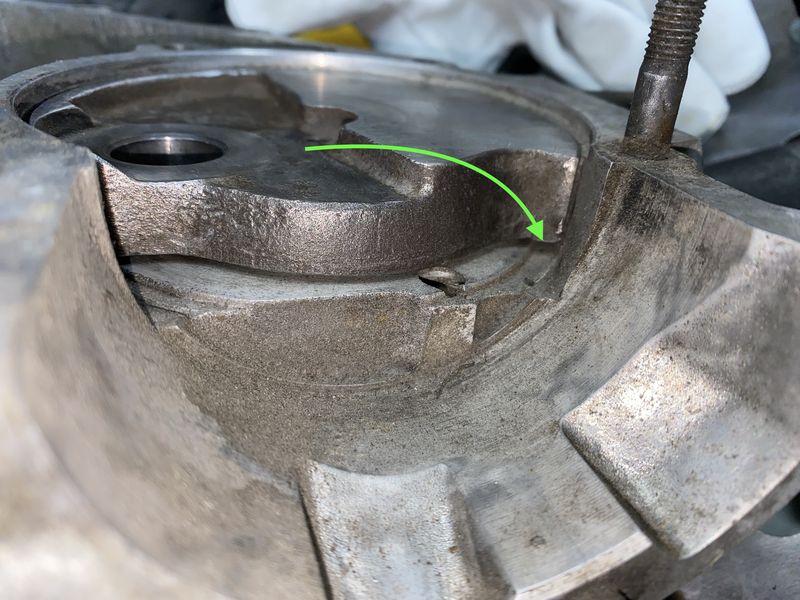
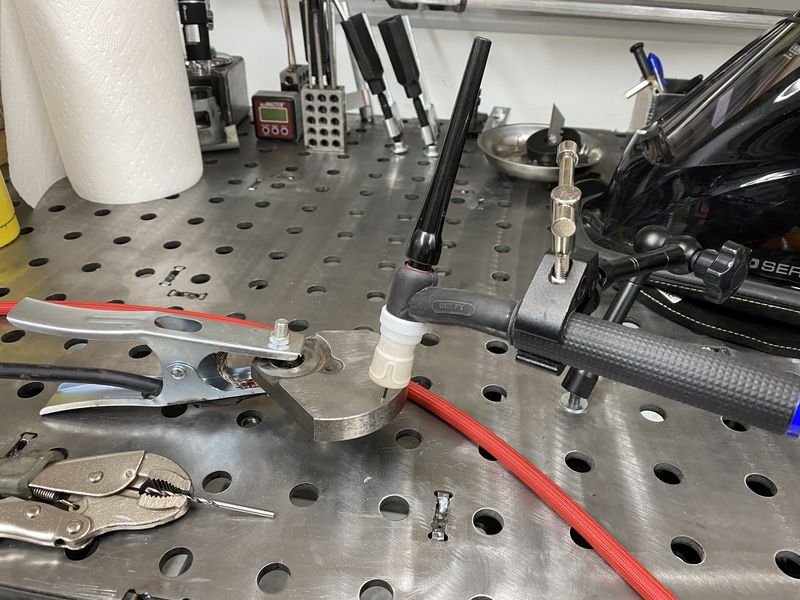
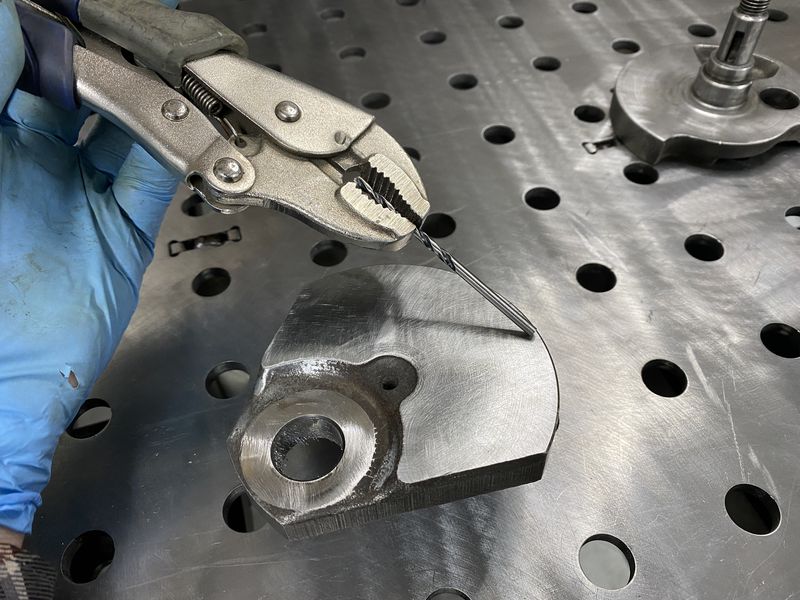
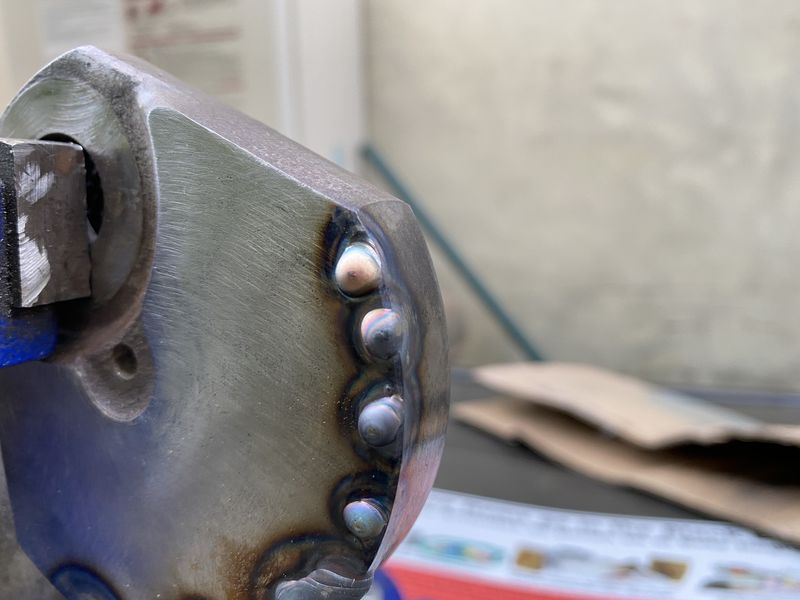
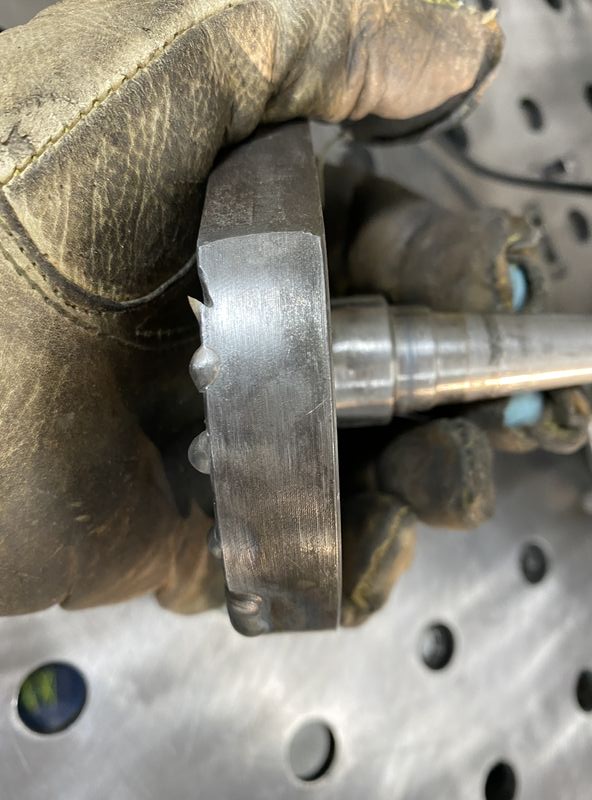
|
|
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
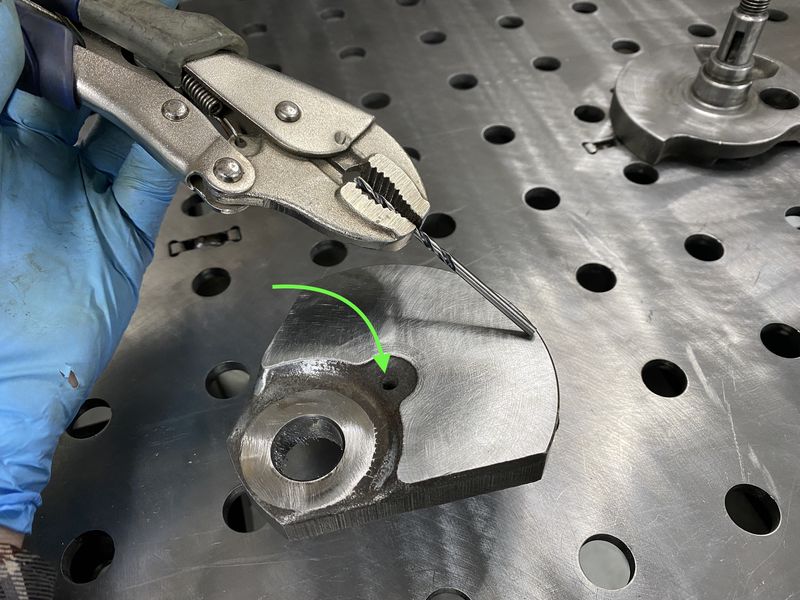
|
Not So Moderator

VNB VSC VSX Li150 09C C125 - (vmb vse v9b)
Joined: UTC
Posts: 10814 Location: Hustletown, TX |

|
bodgemaster

63 GL, 76 Super (x2), 74 Primavera (x2), 79 P200, 06 Fly 150
Joined: UTC
Posts: 7949 Location: So Cal |
|
|

|
Veni, Vidi, Posti

79 P200E (Ruby), 62 Allstate (B-62), 63 VBB (Storm)
Joined: UTC
Posts: 5296 Location: Florence, OR |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
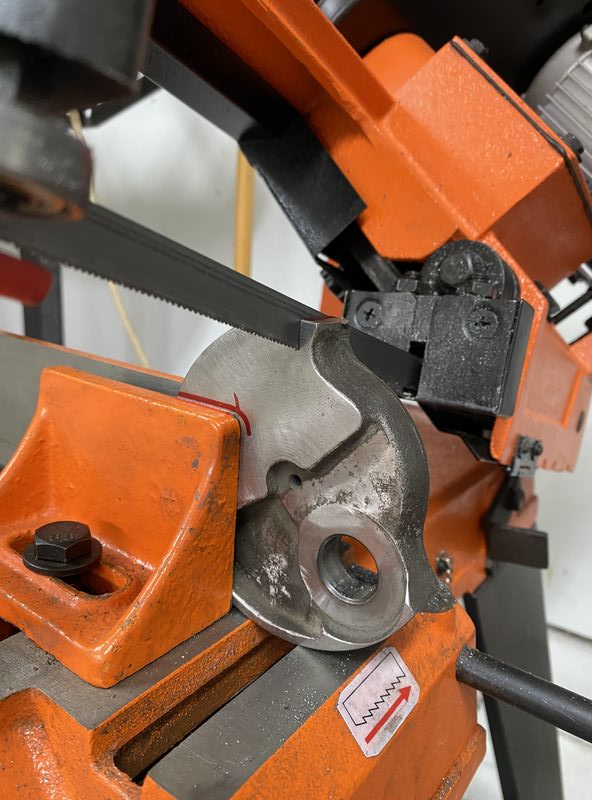
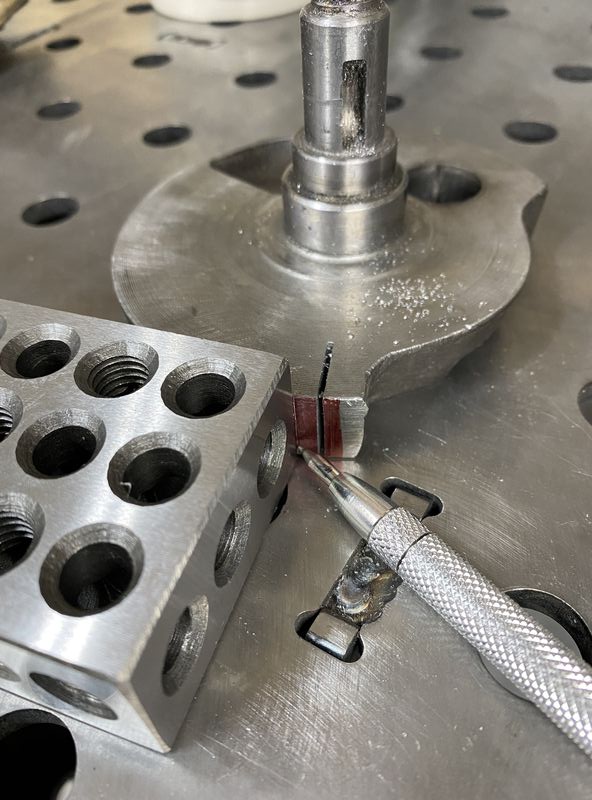
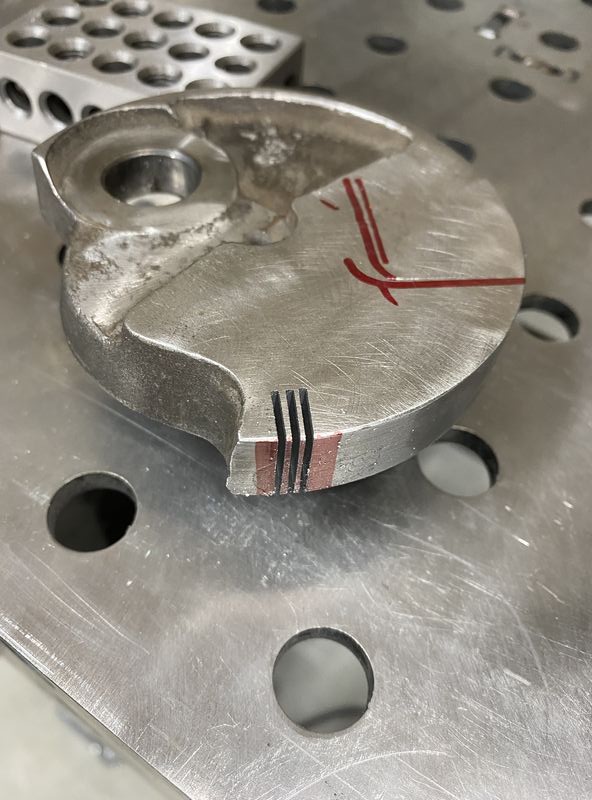
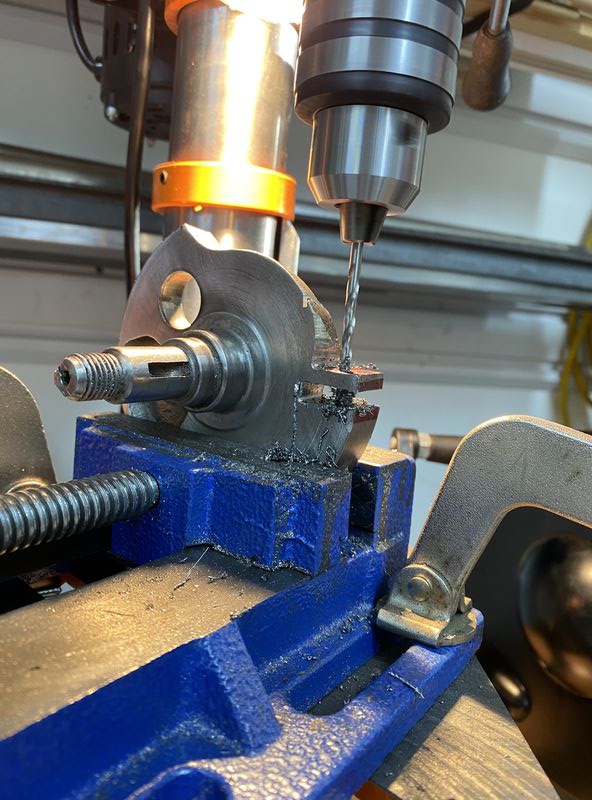
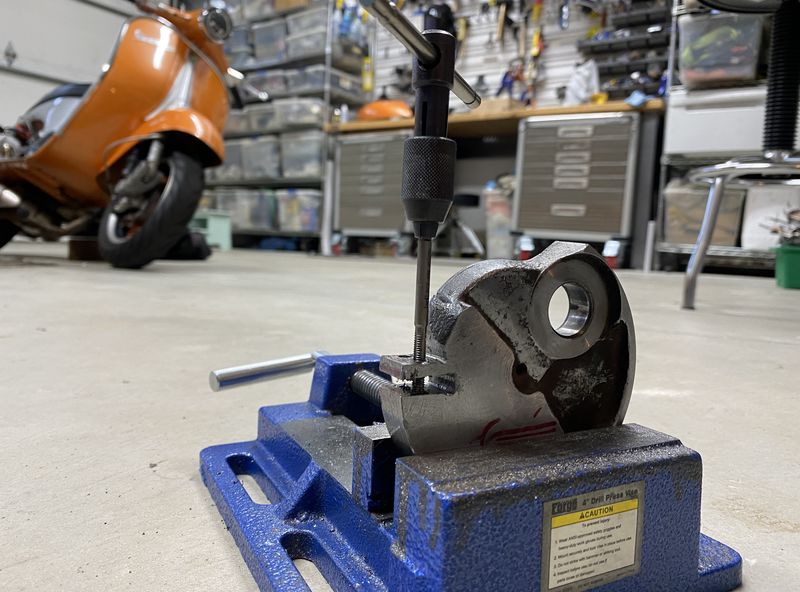
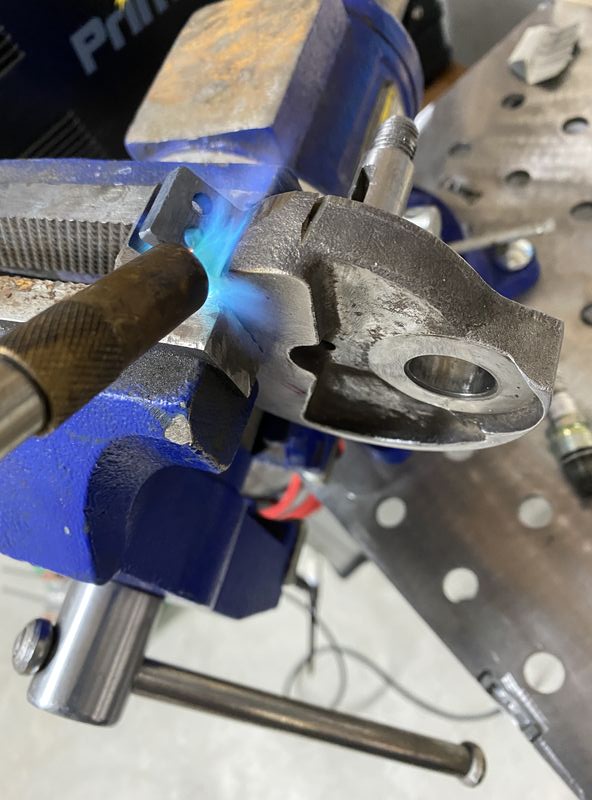
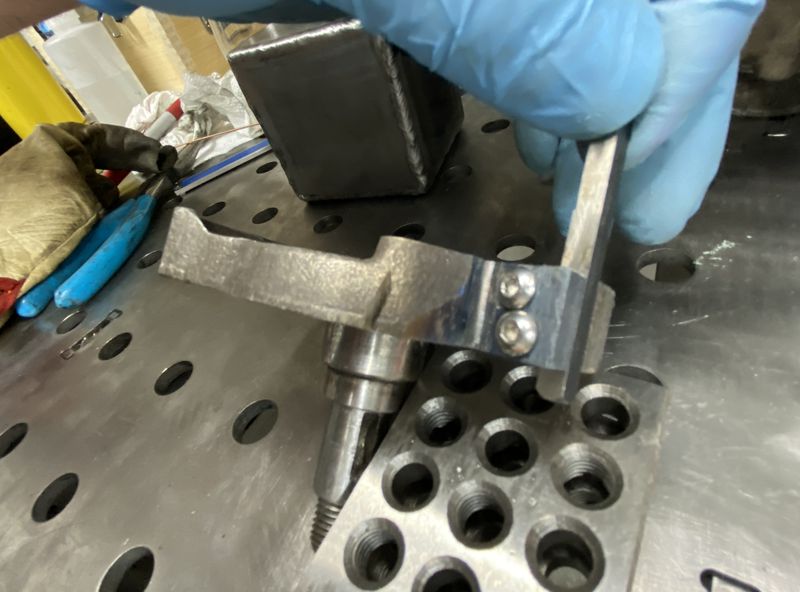
|
|
|
bodgemaster
63 GL, 76 Super (x2), 74 Primavera (x2), 79 P200, 06 Fly 150
Joined: UTC
Posts: 7949 Location: So Cal |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
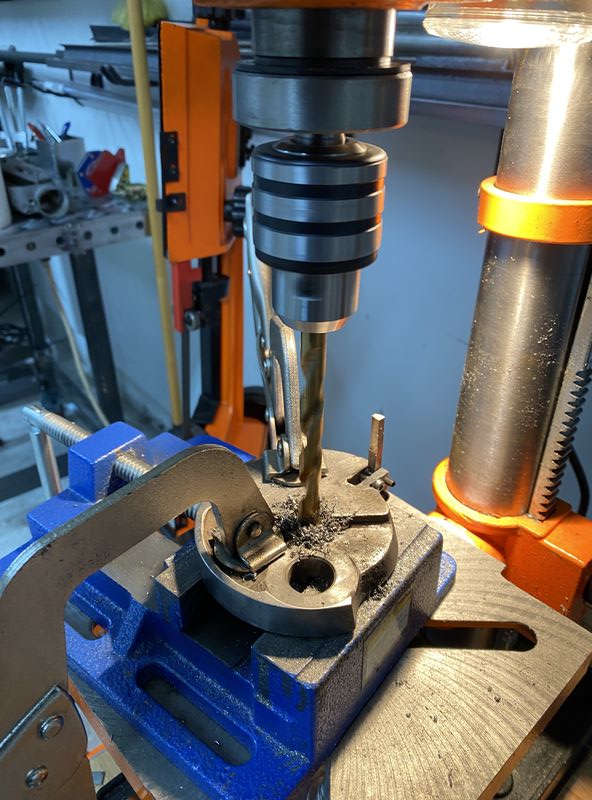
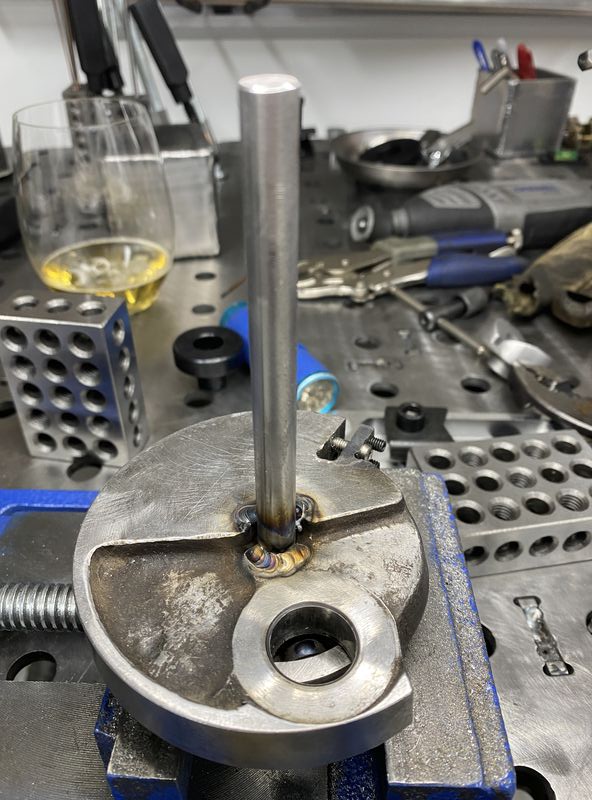
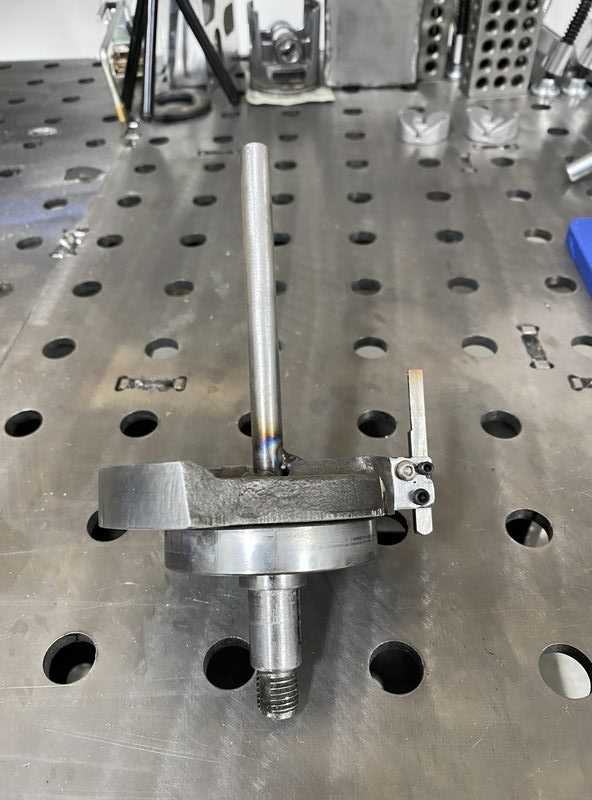
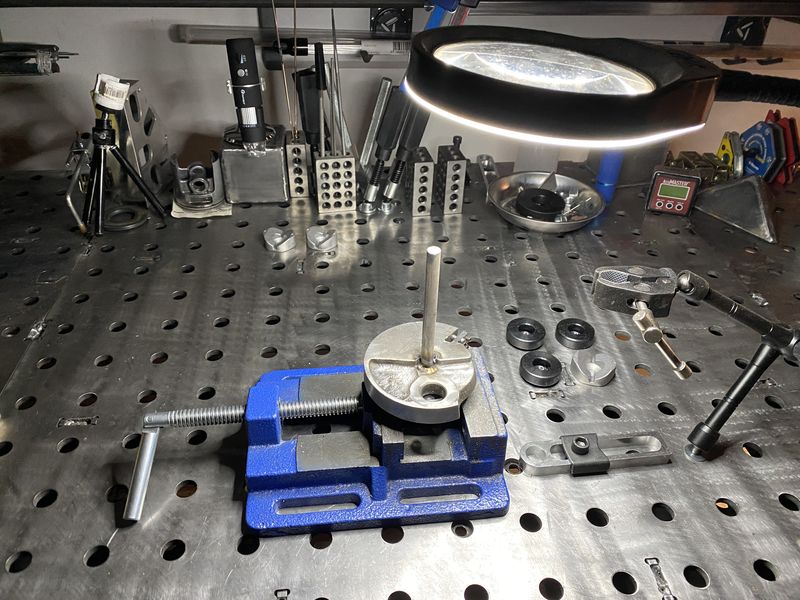
|
bodgemaster
63 GL, 76 Super (x2), 74 Primavera (x2), 79 P200, 06 Fly 150
Joined: UTC
Posts: 7949 Location: So Cal |
|
|

|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
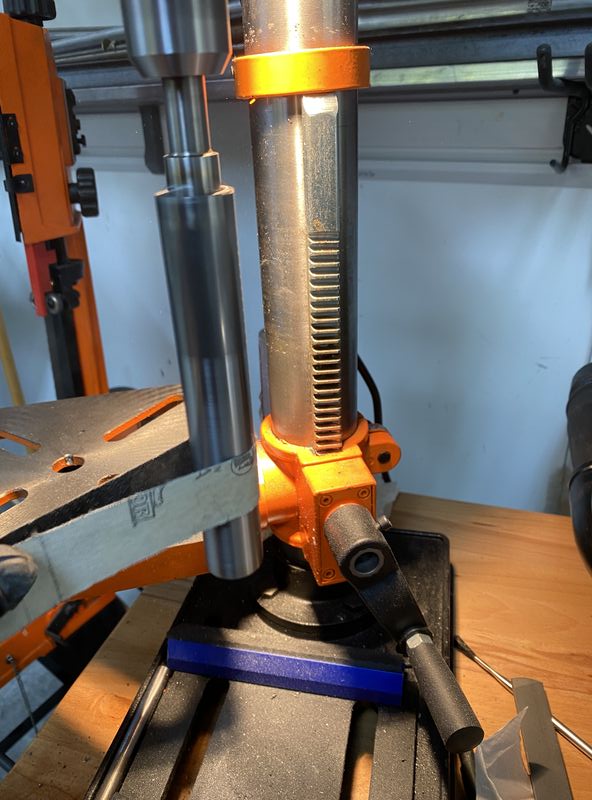
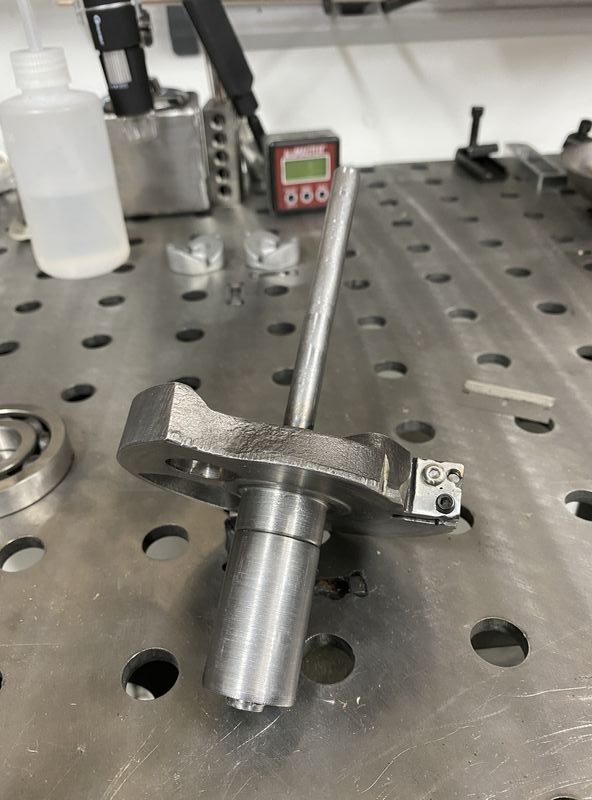
|
|
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
|

|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
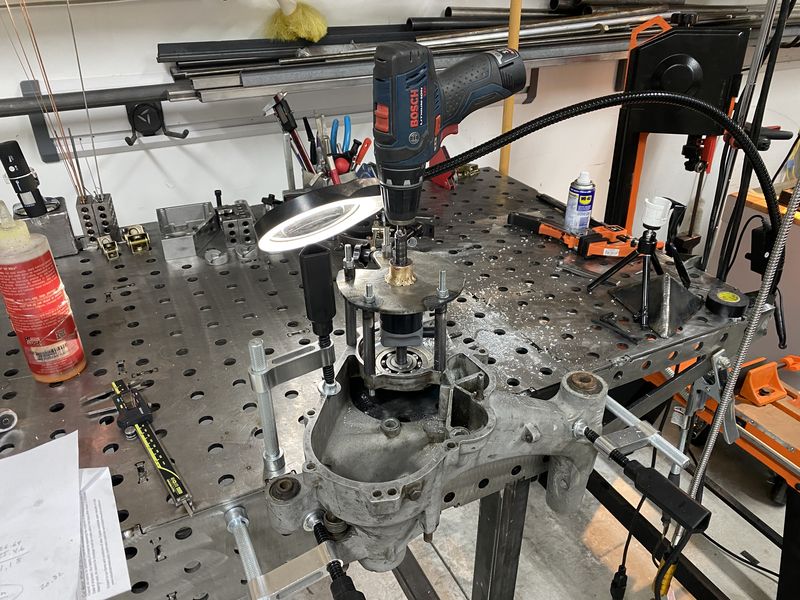
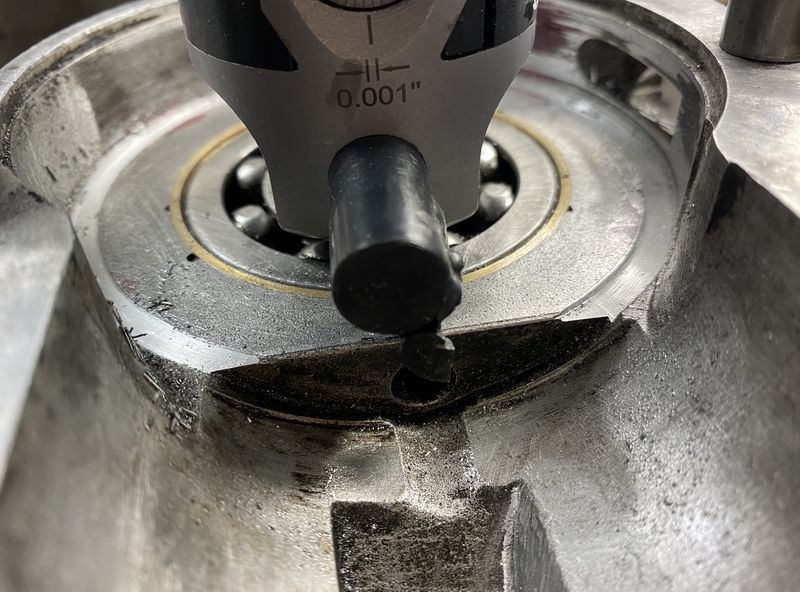
|
|
|
|

|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
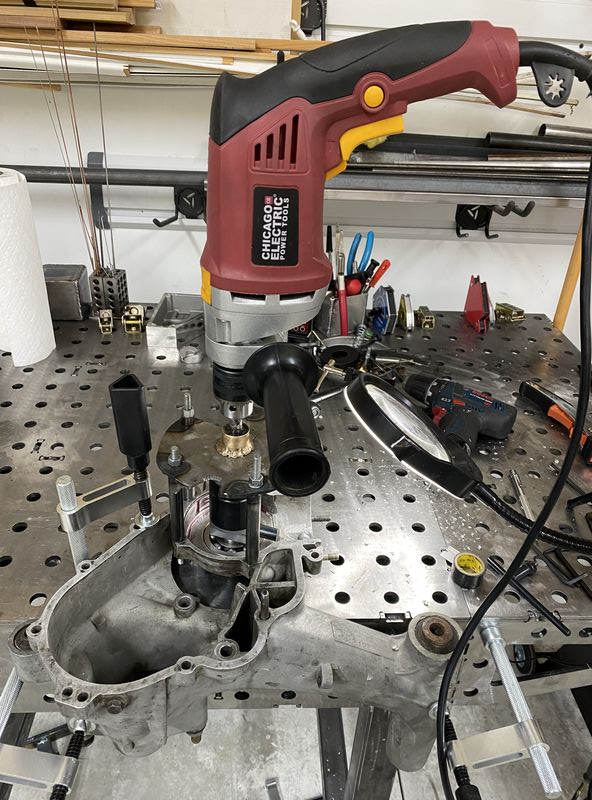
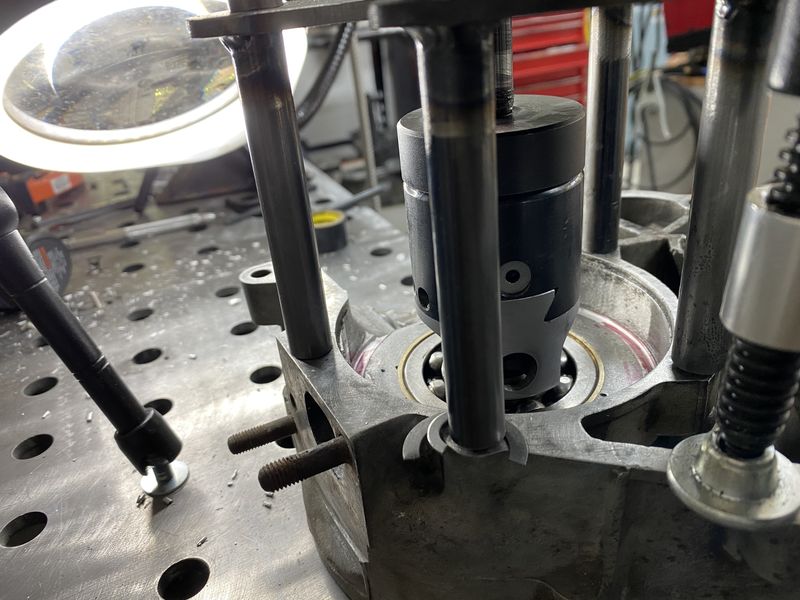
|
|
|
|
|
Not So Moderator
VNB VSC VSX Li150 09C C125 - (vmb vse v9b)
Joined: UTC
Posts: 10814 Location: Hustletown, TX |
|
Ossessionato

P208, Stella VMC Stelvio 187, Stella 150, VNX1T, V9A1T, V9B1T, 02 Sportster XLH1208
Joined: UTC
Posts: 4110 Location: Staten Island, NY |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
bodgemaster
63 GL, 76 Super (x2), 74 Primavera (x2), 79 P200, 06 Fly 150
Joined: UTC
Posts: 7949 Location: So Cal |
|
Not So Moderator
VNB VSC VSX Li150 09C C125 - (vmb vse v9b)
Joined: UTC
Posts: 10814 Location: Hustletown, TX |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
|
|
|

|
Innovator
63 GL, 62 VBB, 05 Stella, 66 Smallstate, 66 Lammy S3, 63 Lammy S3 Riverside
Joined: UTC
Posts: 13192 Location: Nashville 359 Days Since Last Explosion |
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
|
|
Nedminder
62 VBB1T Round Tail W/ leaner sidecar
Joined: UTC
Posts: 4905 Location: california |
|
Not So Moderator
VNB VSC VSX Li150 09C C125 - (vmb vse v9b)
Joined: UTC
Posts: 10814 Location: Hustletown, TX |
Modern Vespa is the premier site for modern Vespa and Piaggio scooters. Vespa GTS300, GTS250, GTV, GT200, LX150, LXS, ET4, ET2, MP3, Fuoco, Elettrica and more.

Shop on Amazon with Modern Vespa
Modern Vespa is a participant in the Amazon Services LLC Associates Program, an affiliate advertising program designed to provide a means for sites to earn advertising fees by advertising and linking to amazon.com
Modern Vespa is a participant in the Amazon Services LLC Associates Program, an affiliate advertising program designed to provide a means for sites to earn advertising fees by advertising and linking to amazon.com
[ Time: 0.0383s ][ Queries: 4 (0.0304s) ][ live ][ 343 ][ ThingOne ]